Materials we manufacture / PETG
PETG CF
Filament guide.
WJ PETG-CF adds chopped carbon fibre to a PETG base, overcoming the relatively low stiffness of standard PETG while keeping the low warping and easy bed adhesion that make PETG popular. The fibre reinforcement raises flexural and tensile performance and gives parts a matte, fibre-textured finish. With a heat deflection temperature of approximately 105 °C at 0.45 MPa, it suits structural, load-bearing parts that need more rigidity than PETG or PLA+ without moving to a high-temperature engineering polymer.
WJ-TDS-PETGCF-001 · Rev V1.0 · Issued 2026-08-01
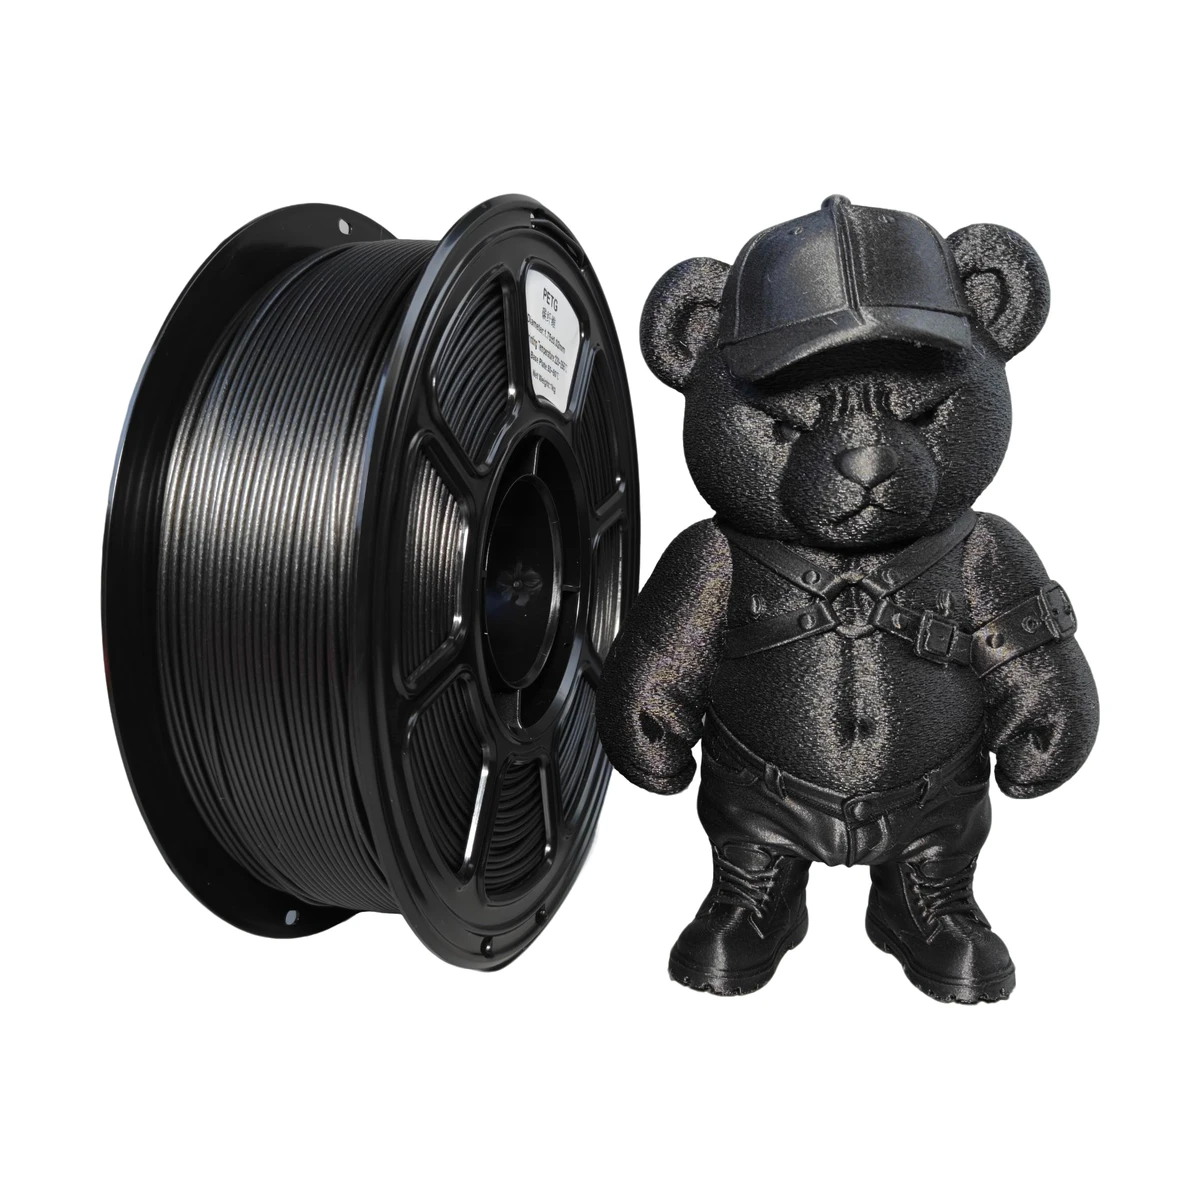
- Nozzle temperature
- 250 – 270 °C
- Bed temperature
- 90 – 110 °C
- Printing speed
- 40 – 150 mm/s
- Enclosed chamber
- Not required
Technical data sheet
Overview & applications.
WJ PETG-CF adds chopped carbon fibre to a PETG base, overcoming the relatively low stiffness of standard PETG while keeping the low warping and easy bed adhesion that make PETG popular. The fibre reinforcement raises flexural and tensile performance and gives parts a matte, fibre-textured finish. With a heat deflection temperature of approximately 105 °C at 0.45 MPa, it suits structural, load-bearing parts that need more rigidity than PETG or PLA+ without moving to a high-temperature engineering polymer.
Typical applications
structural brackets and enclosures, drone frames, jigs and fixtures, and functional prototypes that need extra stiffness over standard PETG while keeping easy, low-warp printing.
Product specifications
| Parameter | Unit | Value |
|---|---|---|
| Filament diameter | mm | 1.75 |
| Diameter tolerance | mm | ± 0.03 |
| Net filament weight | kg | 1 |
| Spool material | · | PC + ABS spool, Ø 200 × 65 mm, hub Ø 55 mm, heat resistant to 90 °C |
| Spool size (Ø × H) | mm | Ø 200 × 65 mm |
| Colour range | · | Stock colours as listed on the product page; RAL / Pantone matching and custom colour development on request |
Technical data sheet
Recommended printing parameters.
Use the grade-specific ranges as a starting point and tune settings for your printer and part geometry.
| Parameter | Unit | Value |
|---|---|---|
| Drying before printing | °C / h | 65 °C for 8 h |
| Printing and storage humidity | · | Dry storage; sealed with desiccant |
| Nozzle size | mm | at least 0.4 (0.6 recommended) |
| Nozzle type | · | Hardened steel / diamond tip (required) |
| Nozzle temperature | °C | 250 – 270 |
| Build plate type | · | Glass or PEI |
| Bed surface preparation | · | Clean; light adhesive if needed |
| Bed temperature | °C | 90 – 110 |
| Part cooling fan | · | Medium to high |
| Printing speed | mm/s | 40 – 150 |
| Enclosed chamber | · | Not required |
| Chamber temperature | °C | 25 – 45 |
| Retraction length / speed | mm / mm/s | 0.6 – 1.0 mm / 20 – 40 mm/s |
| Max overhang angle | ° | ~ 70 |
| Max bridging length | mm | ~ 30 |
This technical data sheet provides typical reference values for material comparison and selection only. It is not an independent third-party test report and does not constitute a product specification, warranty or guarantee of performance. Test methods and specimen conditions are stated in the corresponding sections. The user must verify suitability for the intended application.
Technical data sheet
Material properties.
Typical values from the original TDS. Preserve the test method and specimen orientation when comparing materials.
Physical & thermal properties
| Property | Test method | Unit | Typical value |
|---|---|---|---|
| Density | ISO 1183 | g/cm³ | ~ 1.25 |
| Melt flow rate (MFR) | 210 °C, 2.16 kg | g/10 min | ~ 1.4 ± 0.2 |
| Melting temperature | DSC | °C | ~ 250 |
| Glass transition temperature | DSC | °C | ~ 80 |
| Vicat softening temperature | ISO 306 | °C | ~ 85 |
| Heat deflection temperature | ISO 75, 0.45 MPa | °C | ~ 105 |
| Heat deflection temperature | ISO 75, 1.8 MPa | °C | ~ 95 |
| Saturated water absorption | 25 °C, 55 % RH | % | ~ 0.3 |
Mechanical properties
| Property | Test method | Unit | Typical value |
|---|---|---|---|
| Young's modulus (X·Y) | ISO 527 / GB/T 1040 | MPa | ~ 2500 ± 150 |
| Young's modulus (Z) | ISO 527 / GB/T 1040 | MPa | ~ 1900 ± 150 |
| Tensile strength (X·Y) | ISO 527 / GB/T 1040 | MPa | ~ 50 ± 4 |
| Tensile strength (Z) | ISO 527 / GB/T 1040 | MPa | ~ 45 ± 4 |
| Elongation at break (X·Y) | ISO 527 / GB/T 1040 | % | ~ 12 |
| Elongation at break (Z) | ISO 527 / GB/T 1040 | % | ~ 6 |
| Flexural modulus | ISO 178 / GB/T 9341 | MPa | ~ 2700 ± 130 |
| Flexural strength | ISO 178 / GB/T 9341 | MPa | ~ 80 ± 5 |
| Impact strength, notched | ISO 179 / GB/T 1043 | kJ/m² | ~ 6.5 |
| Impact strength, unnotched | ISO 179 / GB/T 1043 | kJ/m² | ~ 16 |
Chemical & physical characteristics
| Parameter | Value |
|---|---|
| Composition | Carbon-fibre reinforced PETG (PETG-CF) |
| Odour | Slight odour when printing |
| Skin hazard | Cut fibre ends can be sharp – gloves recommended |
| Chemical stability | Stable under normal storage and handling |
| Solubility | Insoluble in water |
| UV and weathering resistance | Moderate – similar to standard PETG |
| Acid resistance | Resistant to dilute acids |
| Alkali resistance | Resistant to dilute bases |
| Organic solvent resistance | Not resistant to some organic solvents |
| Oil and grease resistance | Resistant to common oils and greases |
| Flammability | Flammable |
| Combustion products | Water, carbon oxides |
N/A values remain as reported. Material-family compatibility statements require application-specific validation.
Technical data sheet
Data source & test conditions.
| Parameter | Unit | Value |
|---|---|---|
| Nozzle temperature | °C | 260 |
| Bed temperature | °C | 100 |
| Printing speed | mm/s | 80 |
| Infill density | % | 100 |
| Layer height | mm | 0.2 |
| Specimen conditioning / annealing | °C / h | 23 °C / 50 % RH for 24 h (ISO 291) |
| Topic | Guidance |
|---|---|
| Typical, not minimum | The property tables describe specimens printed exactly as stated in Section 5. They describe the material, not a machined or moulded part. |
| Orientation matters | Values marked X·Y apply to specimens printed flat on the build plate. Z values are measured on parts printed standing up and are typically lower than X·Y. Design for the direction that carries the load. |
| Batch variation | Values carry a ± range where extrusion, pigment and ambient humidity vary between batches; colour masterbatch can shift impact strength noticeably. Where no deviation is given, the value is a single representative test. |
| Not a certificate | This sheet is not an inspection certificate, a Declaration of Conformity, or a certificate of analysis. Batch-specific CoA, RoHS / REACH declarations and safety data sheets are issued separately on request. |
Technical data sheet
Storage, handling & safety.
| Topic | Guidance |
|---|---|
| Storage before use | Sealed bag with desiccant, 15 – 25 °C, below 50 % RH, away from direct sunlight and UV, away from ignition sources. Shelf life 24 months. |
| Storage after opening | Engineering grades absorb moisture noticeably. Reseal with desiccant and re-dry before critical prints: 70 – 80 °C for 4 – 6 h. |
| Symptoms of moisture | Popping and hissing at the nozzle, steam bubbles, rough extrusion, weak layer bonding, loss of impact strength. Dry the spool before changing settings. |
| Handling | Keep the spool on its holder and avoid sharp bends at the extruder inlet. Store away from solvents and strong oxidisers. |
| Ventilation | Printing releases a noticeable styrene or solvent-type odour and measurable VOC. Print in a well-ventilated area, preferably under extraction or with a filtered enclosure. Not for use in enclosed occupied spaces. |
| Fire and disposal | Combustible solid. Keep away from open flame and hot surfaces above 300 °C. Spool, bag and carton are recyclable; offcuts are not biodegradable. Provide adequate ventilation in case of fire – combustion yields carbon oxides. |
| Personal protection | No special protection required for normal use. Wear gloves when handling hot parts and safety glasses when cutting filament. For prolonged printing in a confined space, use an organic-vapour respirator. |
Technical data sheet
OEM & ordering.
| Topic | Ordering information |
|---|---|
| Standard spool | 1.00 kg net, Ø 200 mm, 68 mm hub bore, 4 locating holes. 0.25 / 0.50 / 3.00 kg spools on request. |
| Standard diameter | 1.75 mm (2.85 mm on request). Tolerance per Section 2. |
| Export carton | 10 rolls per carton, 5-ply corrugated. Carton net 10.0 kg, gross approx. 13.1 kg. Neutral print as standard. |
| Colour range | Stock colours as listed in Section 2. Custom colours matched to RAL, Pantone or a physical sample, subject to a minimum batch quantity. |
| OEM services | Spool label, shrink film print, spool material and colour, carton artwork and user manual. Artwork setup and MOQ are quoted per project. |
| Order confirmation | Every order is confirmed by a proforma invoice stating grade, colour, diameter, quantity, unit price, Incoterms and lead time. |
| Shipping and quality documents | Commercial invoice, packing list, bill of lading, certificate of origin and batch certificate of analysis as standard. RoHS / REACH declaration and safety data sheet on request. |
Confirm current commercial terms with WJ for your project.
Data disclosure
Disclaimer & data status.
The data in this document are typical values obtained from tests on standard specimens produced under the conditions described in Section 5. They are provided for material comparison and selection only and do not constitute a specification, warranty or guarantee of performance. Properties of an actual printed part depend on printer hardware, slicing parameters, part geometry, build orientation, ambient conditions and post-processing. WJ reserves the right to amend this document without notice. The buyer is responsible for verifying that the material is suitable for the intended application, including any regulatory or food-contact requirement.
Typical reference values / no third-party report
This technical data sheet provides typical reference values for material comparison and selection only. It is not an independent third-party test report and does not constitute a product specification, warranty or guarantee of performance. Test methods and specimen conditions are stated in the corresponding sections. The user must verify suitability for the intended application.
PDF disclosure addendum A1 · 2026-08-01. Numerical properties and processing ranges are unchanged.
Technical data sheet
Original TDS & revision.
| Rev | Date | Description | Approved |
|---|---|---|---|
| V1.0 | 2026-08-01 | First issue of PETG-CF technical data sheet. | QC / WJ |
Document WJ-TDS-PETGCF-001. This TDS is not a batch certificate of analysis or conformity.
Continue exploring
More in the PETG range.
Manufactured for your brand
Build your PETG CF filament range.
Discuss colours, spool options, labels and packaging with our team. Share your material, quantity and destination for an OEM quote.